
Aboriginal Plant Resins Compared with Modern Polymer Adhesives
Explore how selected Aboriginal plant resins are used as adhesives and compare their composition, processing, and properties with modern EVA polymers. Learn how molecular structure, heating, adhesion, and durability determine how these materials perform.
A stone cutting edge fixed to a wooden handle has a difficult job. The join must withstand knocks, hold two different materials together, and resist moisture. Yet the adhesive also needs to be soft enough to shape around the join during construction.
How can the same material be soft and workable when heated, but hard and durable once it cools?
Aboriginal plant-resin adhesives provide a fascinating example of how chemical composition and material structure determine practical properties. By comparing selected spinifex and grass-tree resins with a modern ethylene-vinyl acetate (EVA) adhesive, we can explore polymer behaviour, thermal softening, adhesion, and durability.
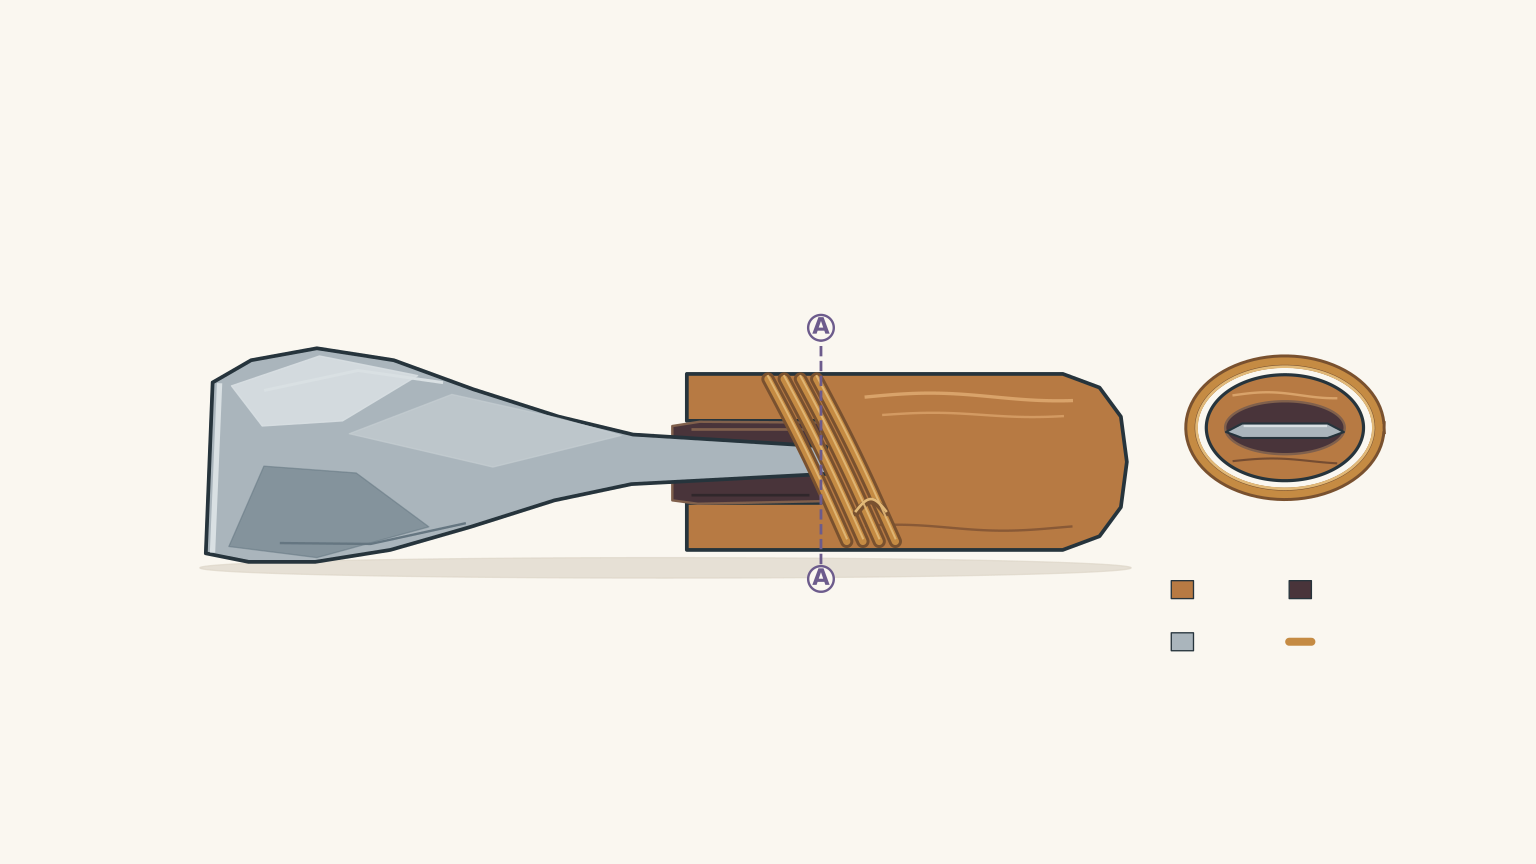
Before looking at the chemistry, make a prediction. If you heat a hardened resin until it becomes workable, then allow it to cool, have you created a new chemical substance?
Usually, the basic heating-and-cooling process involves a physical change. Heating allows the material to soften and become mouldable. Cooling reduces the mobility of its molecules, allowing the material to harden again.
However, this explanation has an important limitation: excessive or repeated heating can also cause irreversible chemical changes. Understanding that distinction is central to comparing natural resins with modern polymers.
01Aboriginal plant resins: different materials, different knowledge
There is no single Aboriginal plant-resin adhesive or universal method of preparing one. Different communities have developed knowledge of the plants and materials available in their own Country, using them for particular purposes.
Two important Australian plant sources are spinifex (Triodia species) and grass trees (Xanthorrhoea species).
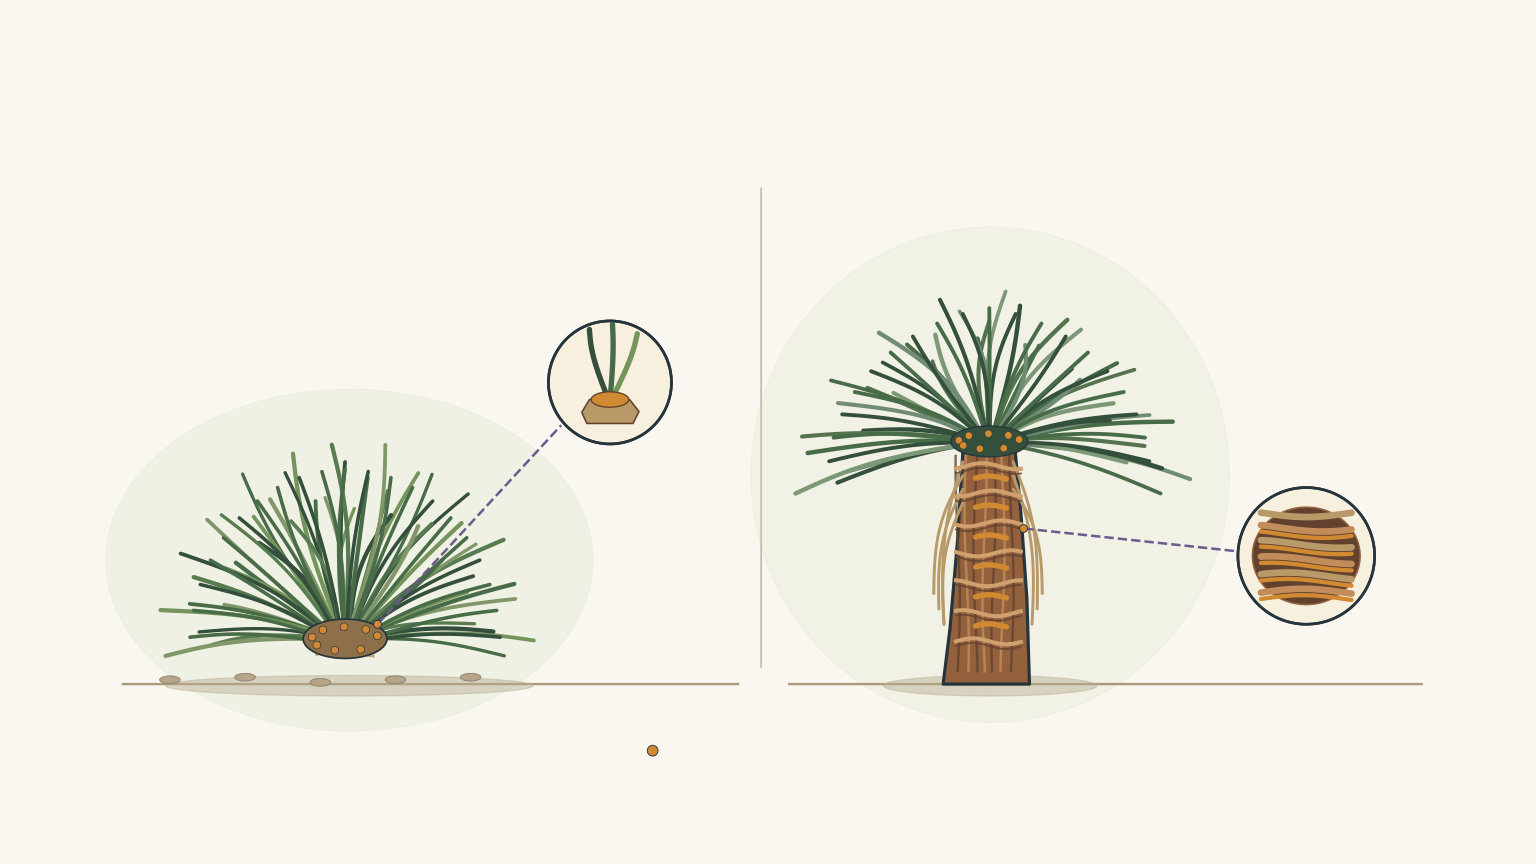
Spinifex resin: Yarnangu and Aṉangu examples
A publicly available Western Australian Department of Education resource documents Yarnangu knowledge shared by Merna Green and local Rangers at the Warburton campus of the Ngaanyatjarra Lands School.
The resource describes the production of kirti, an adhesive obtained from tjanpi spinifex. Resin particles are separated from the plant material and heated carefully until they fuse into a workable substance. Once cooled, the adhesive becomes hard and is used for joining materials in tools and weapons.
This is a particularly useful chemistry example because the material changes its physical properties during heating and cooling without requiring a conventional chemical curing process.
A separate example is documented by Parks Australia at Uluṟu-Kata Tjuṯa. Aṉangu use spinifex resin to make an adhesive called kiti, which is used for repairing, waterproofing, and assembling tools and artefacts. The public account also describes the use of sand in the adhesive.
These examples demonstrate related uses of spinifex resin, but they should not be treated as identical practices. They belong to different communities and knowledge contexts.
Grass-tree resin: Yidinji and Ngarrindjeri examples
Grass trees provide another source of adhesive material.
The Yidinji people of North Queensland are publicly documented as using grass-tree resin in combination with other materials, including native bee wax and mineral substances, to produce a cement-like adhesive.
Kamilaroi author Corey Tutt also describes this example in his article The First Scientists, published by Common Ground.
The Ngarrindjeri Peoples of the Murray River region provide another example. An Australian Curriculum background resource documents their use of grass-tree resin mixed with sand to attach sharp quartz tips to spears.
The important point is that the resin is not necessarily used alone. Other materials can change its physical properties and improve its performance for a particular application.
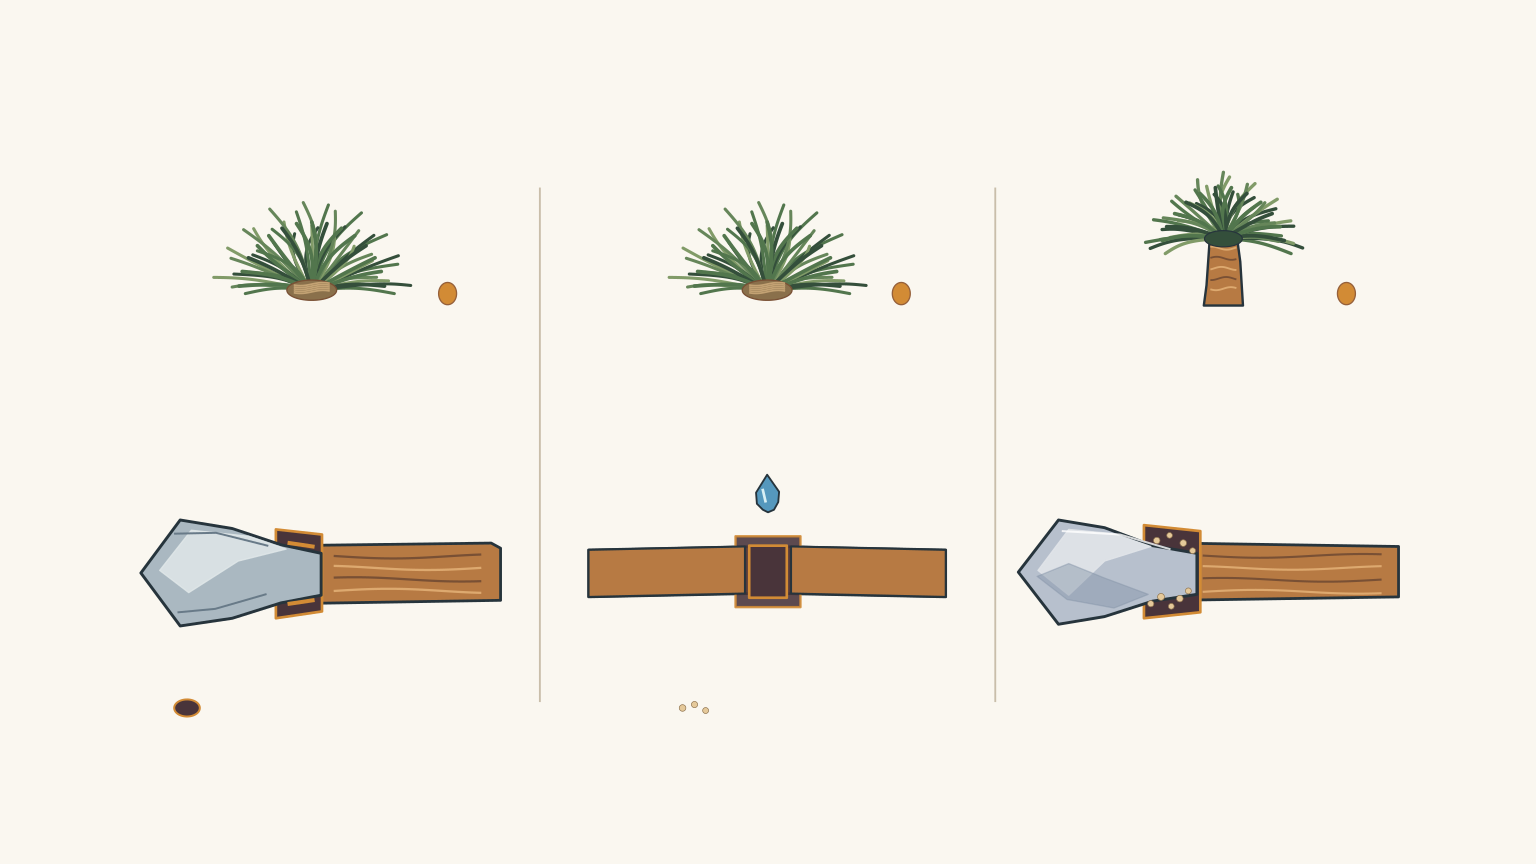
These examples also introduce an important materials-science idea: a useful adhesive does not have to be a single pure substance.
02Why does resin become a useful adhesive?
Imagine trying to attach a small stone to a piece of wood using a hard lump of resin.
If you simply place the lump between the two surfaces, it will not necessarily form a strong join. The adhesive needs to make close contact with both materials.
This requires two important properties:
- The adhesive must be able to spread across the surfaces and enter small gaps.
- Once applied, it must develop enough internal strength to hold the materials together.
Heating helps achieve the first requirement.
As resin warms, its molecules and molecular components gain mobility. The material becomes softer and more capable of changing shape. It can then make closer contact with the wood and stone.
When the resin cools, its mobility decreases and it becomes more rigid.
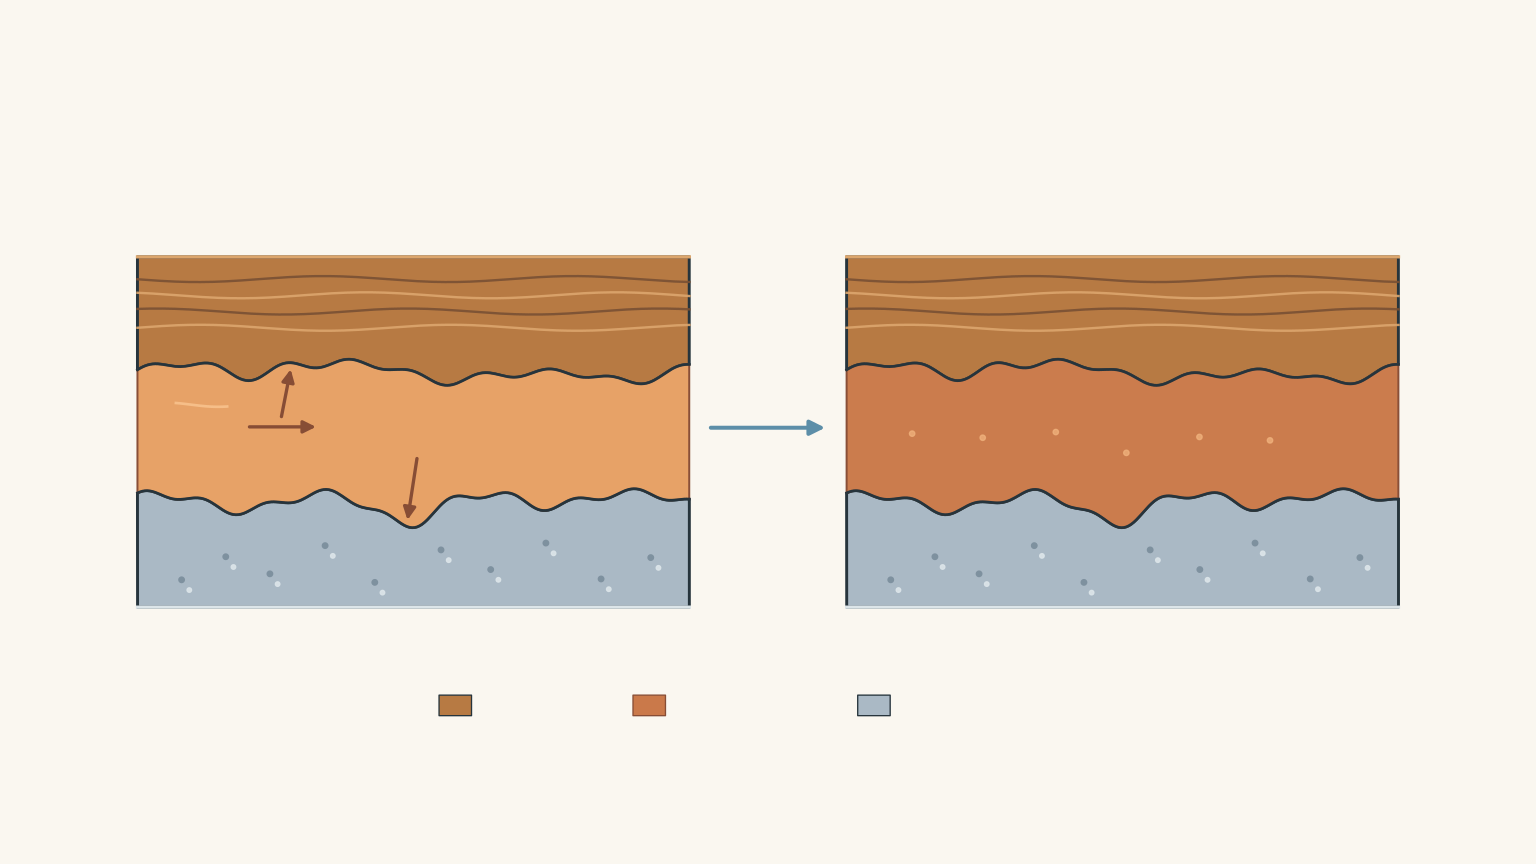
Adhesion versus cohesion
These two words are easy to confuse, but they describe different interactions.
Adhesion is the attraction between different materials. In this example, it describes the interactions between the resin and the wood, and between the resin and the stone.
Cohesion is the attraction between particles within the adhesive itself. It explains why the resin remains together rather than separating into individual pieces.
A successful adhesive needs both.
Adhesion can involve intermolecular attractions, including dispersion forces and dipole interactions. Depending on the materials involved, other interactions may also contribute.
Mechanical interlocking is another important mechanism. When softened adhesive flows into tiny surface irregularities, it can become physically locked into place as it hardens.
Not every adhesive needs to form new covalent bonds with the materials it joins.
This distinction is important. The covalent bonds within a polymer chain can be very strong, but that does not automatically mean the polymer forms covalent bonds with the wood or stone.
The overall strength of the join depends on both adhesion at the interfaces and cohesion within the adhesive.
03Natural resin is not necessarily a single polymer
This is where the chemistry becomes particularly interesting.
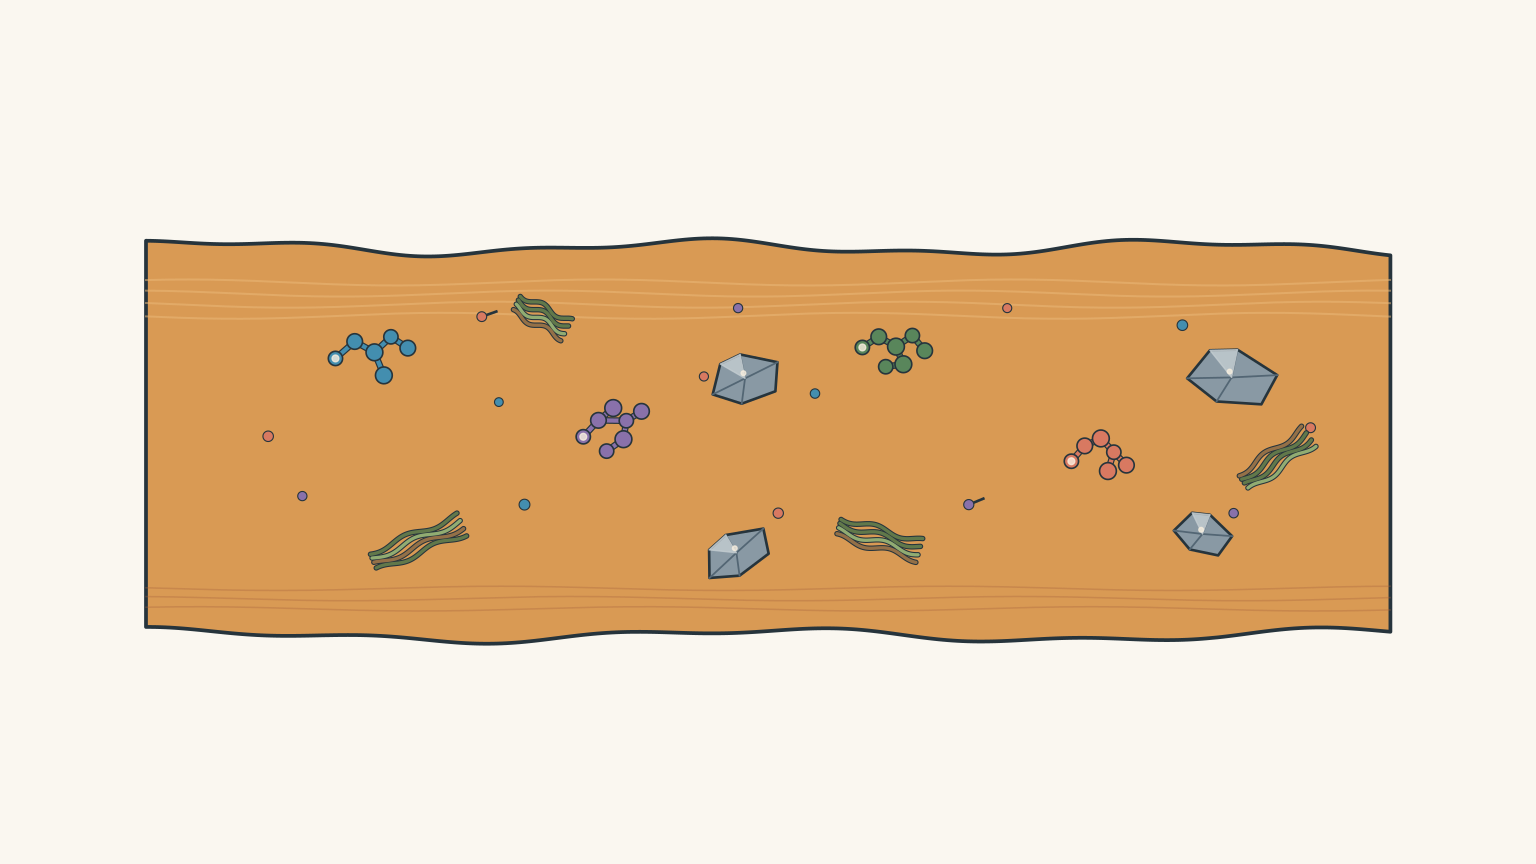
You might expect plant resin to be one large polymer molecule, similar to a synthetic plastic. However, natural resin is often a complex mixture of different chemical compounds.
The word resin describes a type of material, not one specific molecular structure.
What is spinifex resin made from?
A scientific investigation by Mondal, Memmott, Wallis, and Martin (2012), published in Materials Chemistry and Physics, examined the composition and thermal properties of resin from Triodia pungens, a resin-producing spinifex species.
The researchers described the extracted resin as primarily containing a mixture of volatile and non-volatile terpenoid compounds and other secondary compounds.
They also identified inorganic elements within the resin.
Importantly, traditionally prepared resin samples contained additional material, including sediment particles and plant fibres.
This means the final adhesive material can contain several different components:
- Resinous organic compounds from the plant.
- Mineral particles, such as sediment or sand.
- Plant fibres and other naturally occurring material.
The proportions and composition can vary.
The researchers describe spinifex resin as a bio-organic polymeric material, but this should not be interpreted as meaning that every molecule in the resin is one identical repeating polymer chain.
Some components are relatively small molecules, while others contribute to the polymer-like behaviour of the material.
Why do the additional materials matter?
Consider the mineral particles in a resin composite.
These particles are called fillers because they occupy space within the main resin material.
They are not necessarily chemically bonded into the resin’s molecular structure.
Instead, they can change how the material behaves physically.
For example, mineral fillers can:
- Increase surface hardness.
- Restrict the movement of molecular components.
- Change the viscosity and flow behaviour of softened resin.
- Alter the temperature at which the material becomes soft.
- Modify the mechanical properties of the final composite.
Plant fibres can also contribute to the physical structure of the material.
Think of the resin as the continuous material holding the composite together, while the particles and fibres modify its properties.
This is a useful example of a composite material: a material made by combining different components to achieve particular properties.
However, adding more filler does not automatically make an adhesive stronger. If there is too much solid material relative to the resin, there may not be enough continuous adhesive phase to maintain a strong join.
The composition has to suit the intended use.
04Why does heating soften resin?
The physical behaviour of many resinous materials can be understood using the concept of the glass transition temperature.
The glass transition temperature, represented by \(T_g\), describes the temperature range over which an amorphous polymer-rich material changes from a hard, glass-like state to a softer, more flexible state.
Below \(T_g\), molecular movement is restricted. The material tends to be rigid and can behave in a brittle manner.
Above \(T_g\), molecular segments become more mobile. The material becomes more flexible and can deform more easily.
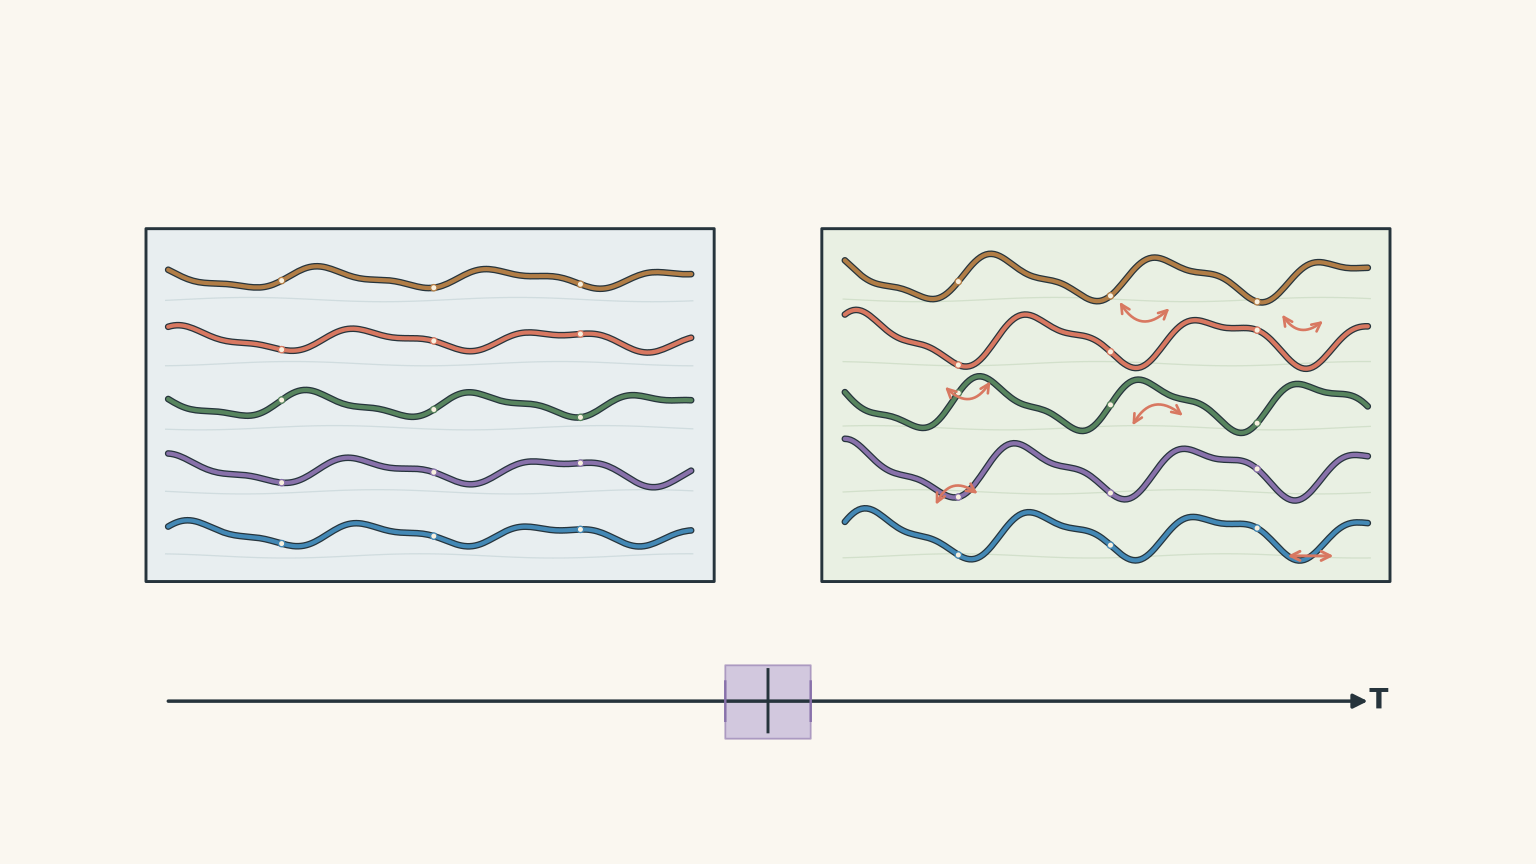
This helps explain why resin can be heated, moulded, and allowed to harden.
However, there is an important distinction.
The glass transition temperature is not the same as the melting point.
A material above its glass transition temperature does not necessarily become a freely flowing liquid. It may simply become softer and more rubber-like.
This distinction matters when describing plant resins because their compositions are complex and their thermal transitions may occur over a range of temperatures.
Processing changes the properties
Heating does more than increase molecular mobility.
The spinifex resin investigation found that the thermal history of a sample influenced its properties.
In particular, heat treatment increased the glass transition temperature of some samples. The researchers associated this with reactions involving functional groups in the resin and the possible formation of a crosslinked network.
The loss of volatile components can also increase the glass transition temperature because these smaller molecules can act as plasticisers, increasing molecular mobility.
Mineral fillers can further restrict molecular movement.
This gives us three important influences on resin behaviour:
| Factor | Effect on material |
|---|---|
| Volatile components | Can increase molecular mobility and lower the glass transition temperature |
| Mineral fillers | Can restrict molecular movement and increase hardness or glass transition temperature |
| Heat treatment | Can cause chemical reactions that change molecular structure and thermal behaviour |
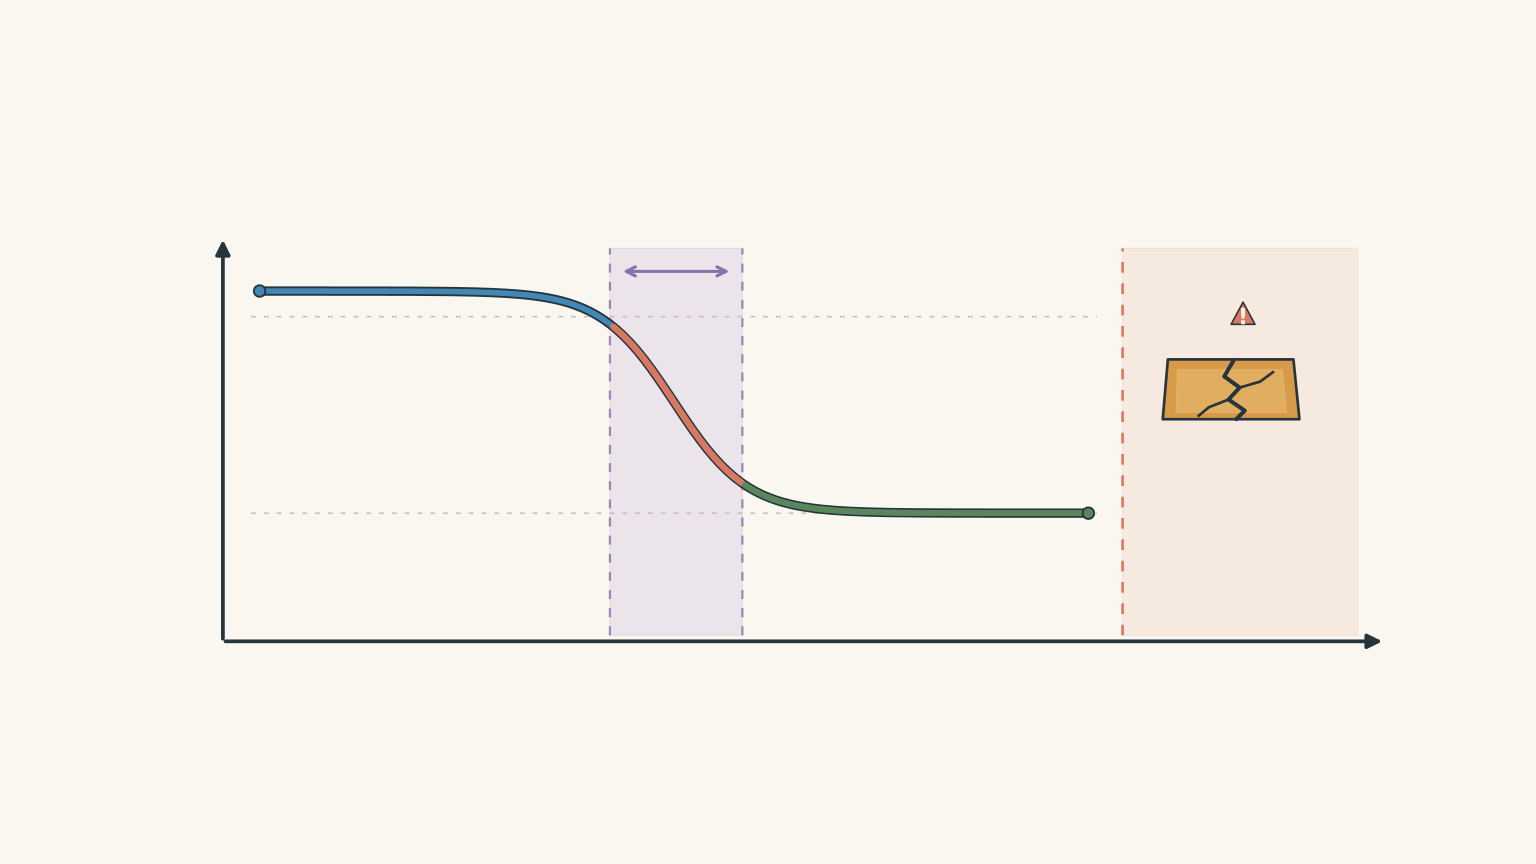
This also explains why repeatedly heating a natural resin does not always restore its original properties.
The first heating cycle might soften the material successfully. However, prolonged or excessive heating can cause irreversible changes, including chemical reactions and thermal degradation.
Some spinifex resins can be reheated successfully, while others become brittle with repeated heating. The Queensland Museum discusses this variation in its article on traditional resin adhesives.
Natural does not automatically mean harmless, either. Some resins are flammable, and excessive heating can damage the material. Their composition and safe handling requirements cannot be assumed from their plant origin.
05Comparing plant resin with a modern polymer: EVA
A useful modern comparison is an ethylene-vinyl acetate (EVA) hot-melt adhesive.
EVA is commonly used in modern adhesives, including some bookbinding and packaging applications.
It is a suitable comparison because, like the plant-resin examples, an EVA hot-melt adhesive can be softened by heating and hardened again by cooling.
However, the molecular structure is quite different.
The structure of EVA
EVA is a copolymer.
A copolymer is a polymer made from two or more different types of monomer.
EVA contains repeating units derived from:
- Ethene, \(\ce{CH2=CH2}\).
- Vinyl acetate, \(\ce{CH2=CHOCOCH3}\).
The resulting polymer contains two different repeating-unit structures along its molecular chains.
The ethylene-derived repeating unit is:
\[ \ce{[-CH2-CH2-]} \]
The vinyl acetate-derived repeating unit is:
\[ \ce{[-CH2-CH(OCOCH3)-]} \]
These units form part of the same copolymer chain.
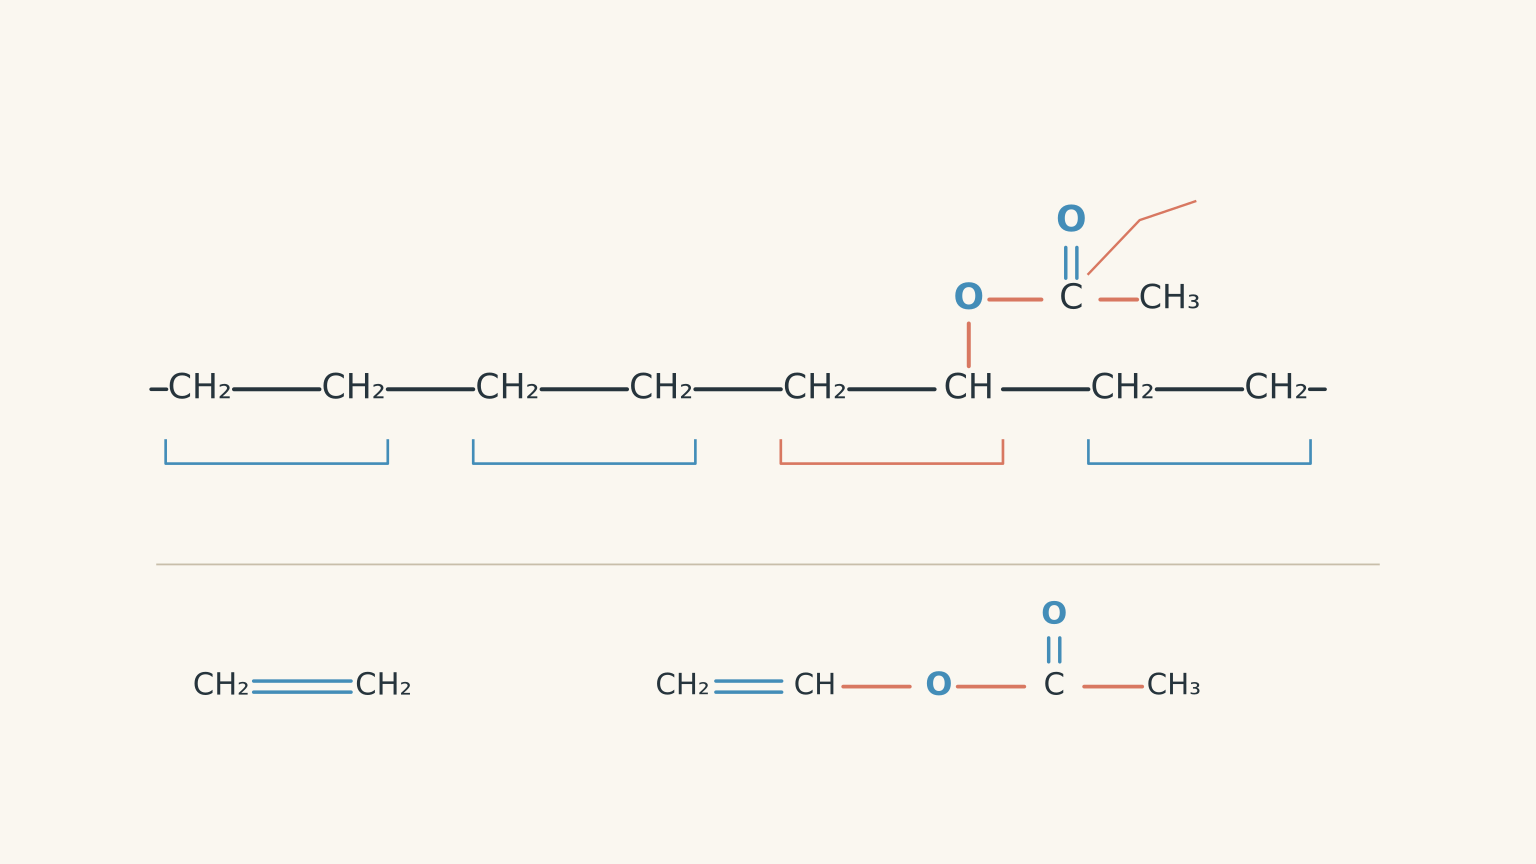
The polymer’s structure helps explain its properties.
The ethylene sections contribute flexible, largely non-polar regions. The vinyl acetate sections introduce polar ester groups, which influence the polymer’s interactions with other materials.
Changing the relative amount of vinyl acetate can influence flexibility, crystallinity, thermal behaviour, and adhesion to different surfaces.
This is one reason polymer manufacturers can adjust EVA formulations for particular applications.
For a refresher on how monomers form polymer chains, see tutorgum’s Monomers vs Polymers: Health and Environmental Impacts.
Why is an EVA hot-melt adhesive not pure EVA?
An important detail is that a commercial hot-melt adhesive is not necessarily made from the polymer alone.
Its formulation can contain several components:
| Component | Main function |
|---|---|
| EVA polymer | Provides the main structure, strength, and flexibility |
| Tackifier resin | Improves initial stickiness and adhesion |
| Wax or plasticiser | Adjusts viscosity, flow, flexibility, and setting behaviour |
| Antioxidant | Helps limit degradation during heating and processing |
The polymer provides the backbone of the adhesive system, while the additional ingredients adjust its performance.
This is surprisingly similar to the general materials-science principle seen in plant-resin composites: the properties of an adhesive depend on the combination of its components, not simply the name of its main material.
How does an EVA hot-melt adhesive set?
The process has three main stages.
1. Heating
The adhesive is heated until it becomes sufficiently soft or molten to be applied.
Its viscosity decreases, allowing it to flow over the surfaces.
2. Application
The molten adhesive spreads across the materials being joined.
It makes close contact with the surfaces and can enter small gaps and irregularities.
3. Cooling
As the adhesive cools, it solidifies.
The polymer chains become less mobile, and the adhesive develops enough cohesive strength to maintain the join.
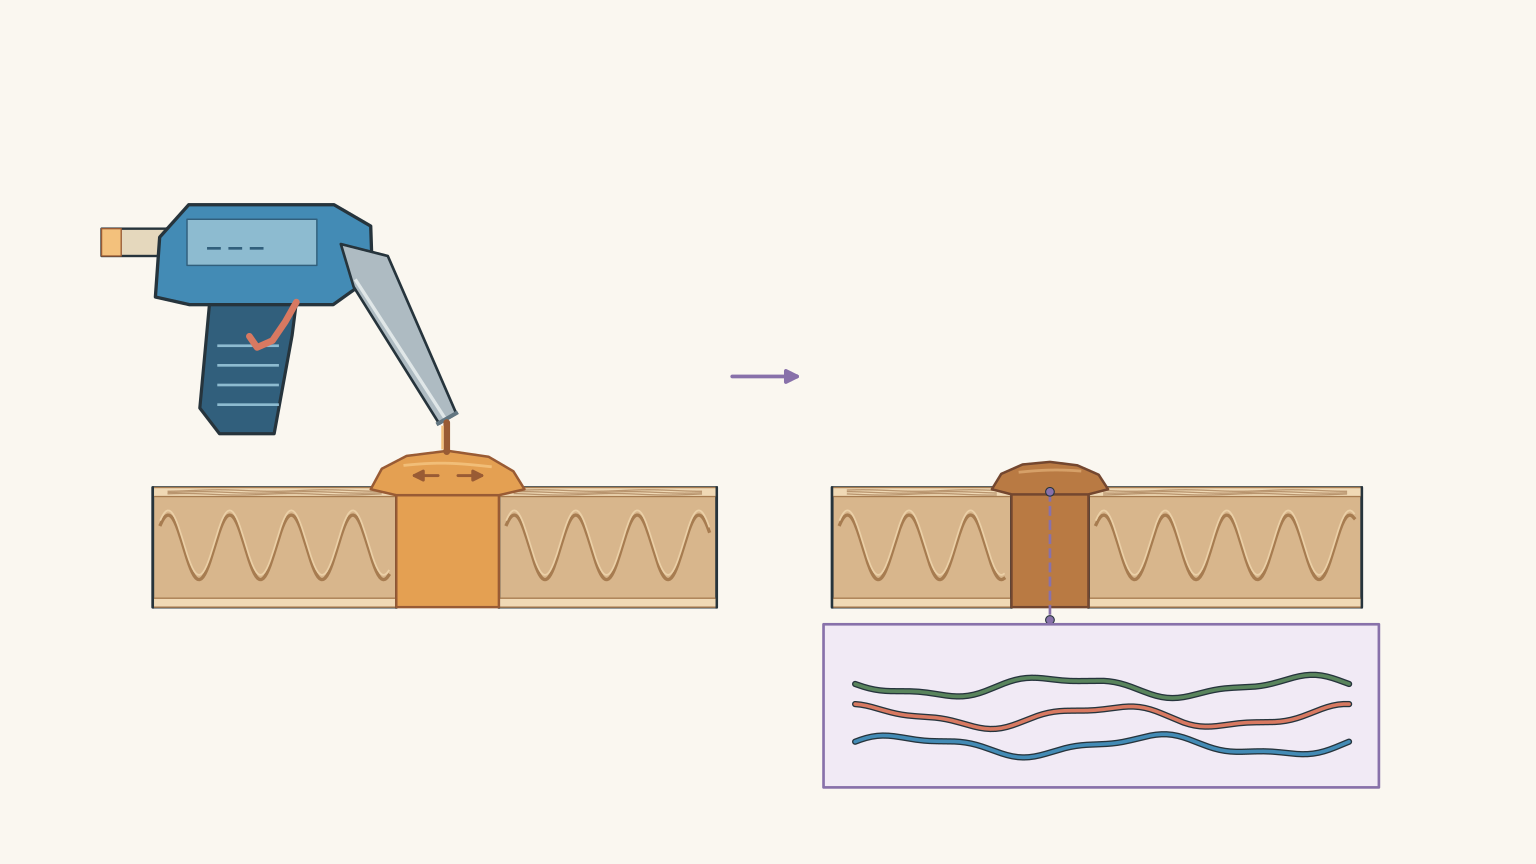
The important point is that ordinary non-reactive EVA hot-melt adhesives set through a physical process.
The polymer does not need to undergo a chemical reaction to form the bond.
This is different from a thermosetting adhesive such as epoxy, where chemical reactions form a crosslinked structure during curing.
Comparing the two materials
| Property | Selected plant-resin adhesives | EVA hot-melt adhesive |
|---|---|---|
| Composition | Complex resinous mixtures, sometimes combined with fillers and fibres | EVA copolymer combined with formulation additives |
| Molecular structure | Variable mixture of organic compounds; some polymer-like fractions | Defined copolymer containing two types of repeating units |
| Processing | Controlled heating makes the material workable | Heating softens or melts the adhesive for application |
| Setting | Cooling allows the resin to harden | Cooling physically solidifies the thermoplastic adhesive |
| Adhesion | Molecular attractions and mechanical interlocking | Molecular attractions and mechanical interlocking |
| Property control | Depends on plant source, composition, and processing history | Formulation can be deliberately adjusted |
| Durability | Some resins provide water-resistant joins, but thermal behaviour varies | Performance depends on formulation, temperature, substrate, and loading |
Neither material is automatically superior.
Plant resins can provide useful combinations of hardness, water resistance, and repairability. Their properties can also be modified by combining them with other materials.
Modern EVA adhesives offer more controlled formulations and predictable processing conditions. However, they can still soften under excessive heat and may deform under sustained loads.
Durability depends on the conditions in which the adhesive is used.
A material that performs well at room temperature may not perform well in a hot environment.
06Worked examples
Worked example: Calculate the mineral filler percentage in a resin composite
A laboratory sample of a plant-resin composite has a total mass of 20.0 g. Analysis shows that 6.0 g of the sample consists of mineral particles.
Calculate the mass percentage of mineral filler.
Step 1
The mass of mineral filler is 6.0 g.
The total mass is 20.0 g.
Step 2
\[ \%\text{ by mass} = \frac{\text{mass of component}} {\text{total mass}} \times 100 \]
Step 3
\[ \begin{aligned} \%\text{ mineral filler} &=\frac{6.0}{20.0}\times100\\ &=30.0\% \end{aligned} \]
Step 4
The sample contains 30.0% mineral filler by mass.
This does not mean that 30.0% of the sample consists of polymer chains. The remaining mass may include resinous organic compounds and plant fibres.
The distinction matters because a composite contains multiple components with different chemical structures and functions.
Worked example: Predict the behaviour of resin above its glass transition temperature
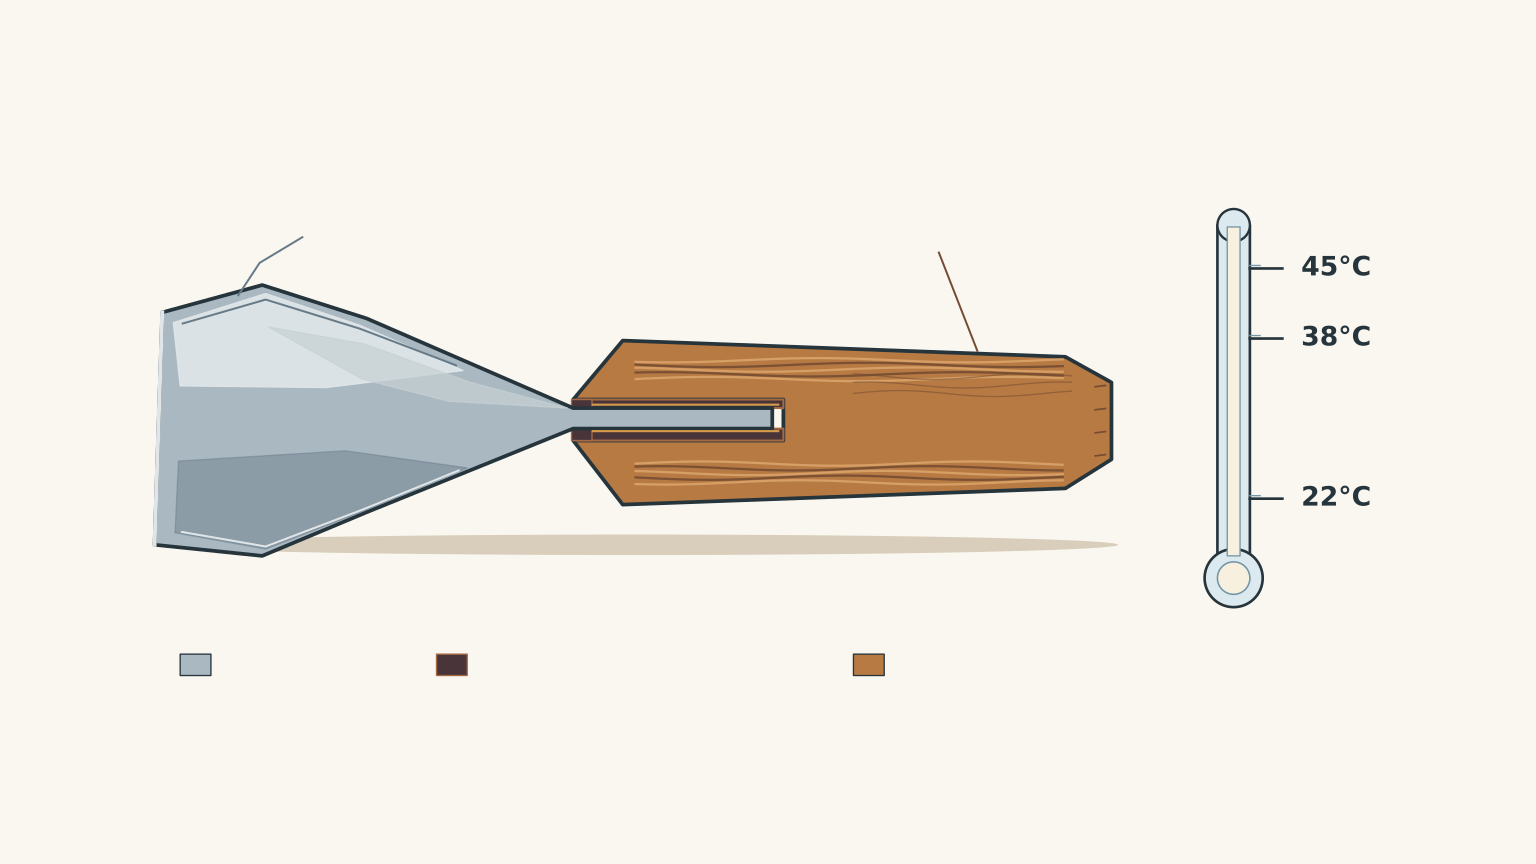
A resin composite has a measured glass transition temperature of 38°C.
A tool containing this adhesive is initially at 22°C. Later, the tool is exposed to sunlight and reaches 45°C.
Predict how the resin’s physical behaviour changes.
Step 1
Initially:
\[ 22^\circ\mathrm{C}<38^\circ\mathrm{C} \]
The resin is below its glass transition temperature.
It is therefore expected to behave in a relatively rigid, glass-like manner.
Step 2
After exposure to sunlight:
\[ 45^\circ\mathrm{C}>38^\circ\mathrm{C} \]
The resin is now above its glass transition temperature.
Its molecular segments have greater mobility, so it becomes softer and more capable of deforming.
Step 3
The adhesive may become less rigid and more susceptible to deformation under an applied load.
This could reduce the stability of the join if the material experiences sustained stress.
Step 4
The resin has not necessarily melted into a liquid.
The glass transition describes a change from glass-like to rubber-like behaviour, not necessarily a complete melting process.
Also, if the resin undergoes chemical degradation during excessive heating, cooling alone may not restore its original properties.
07Questions and solutions
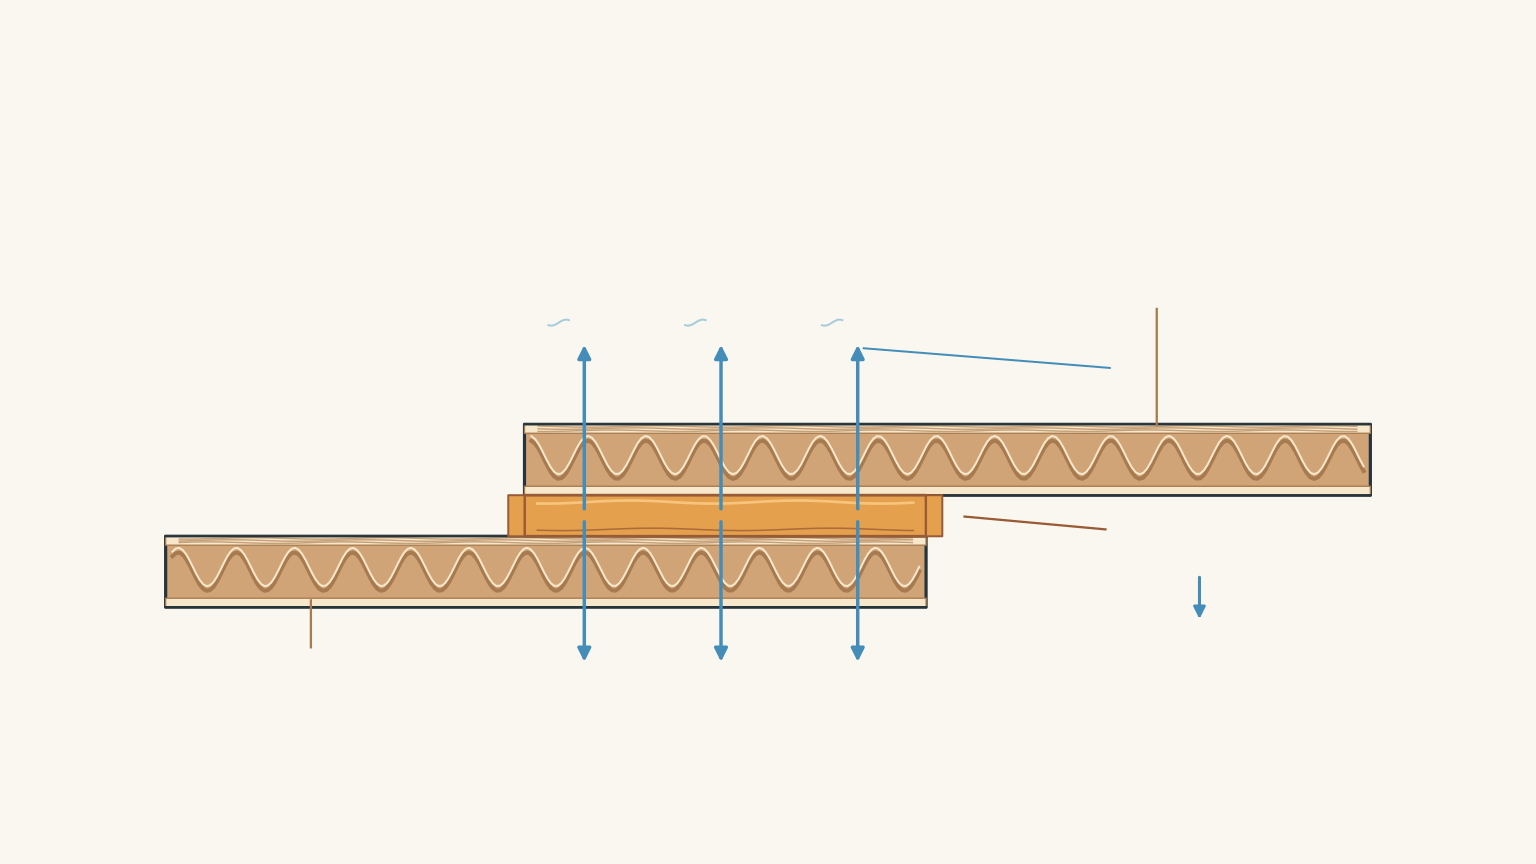
Question 1
An EVA-based hot-melt adhesive is heated and applied between two pieces of cardboard. After the adhesive cools, the cardboard pieces remain attached.
Explain why this process is classified as a physical change rather than a chemical curing reaction.
Solution 1
The adhesive undergoes a physical change during setting, rather than requiring a chemical curing reaction.
When the EVA adhesive is heated, its polymer chains gain mobility and the material becomes sufficiently soft or molten to flow across the cardboard surfaces.
This allows the adhesive to make close contact with both surfaces.
As the material cools, the polymer becomes solid again. Its molecular mobility decreases, and the adhesive develops sufficient cohesive strength to hold the cardboard together.
The chemical structure of the EVA polymer does not need to change during this process.
This is characteristic of a thermoplastic material.
A thermoplastic can soften when heated and become rigid again when cooled, provided it has not undergone irreversible chemical degradation.
Question 2
A scientific investigation of Triodia pungens resin reports the following midpoint glass transition temperatures for two samples:
| Sample | Description | Midpoint \(T_g\) |
|---|---|---|
| SR2 | Threshed resin sample | 8.64°C |
| MR | Museum resin composite containing mineral fillers | 43.44°C |
(a) Calculate the difference between the two glass transition temperatures.
(b) Predict the likely physical behaviour of each sample at 25°C.
(c) Explain why the difference cannot automatically be attributed entirely to the presence of mineral fillers.
Solution 2
The museum composite has a glass transition temperature 34.80°C higher than the threshed resin sample. At 25°C, the two samples are expected to exhibit different physical behaviour.
(a) Calculate the temperature difference.
Use:
\[ \Delta T_g=T_{g,\mathrm{MR}}-T_{g,\mathrm{SR2}} \]
Substitute:
\[ \begin{aligned} \Delta T_g &=43.44-8.64\\ &=34.80^\circ\mathrm{C} \end{aligned} \]
The difference is 34.80°C.
(b) Predict the behaviour at 25°C.
For SR2:
\[ 25^\circ\mathrm{C}>8.64^\circ\mathrm{C} \]
The sample is above its midpoint glass transition temperature.
It is therefore expected to have relatively greater molecular mobility and more rubber-like behaviour.
For MR:
\[ 25^\circ\mathrm{C}<43.44^\circ\mathrm{C} \]
The sample is below its midpoint glass transition temperature.
It is therefore expected to behave more like a rigid, glassy material.
(c) Explain the influence of composition and processing.
It would be tempting to conclude that mineral fillers alone caused the higher glass transition temperature.
However, this conclusion is not justified.
The samples differ in their composition and processing history. Mineral fillers can restrict molecular movement, but heat treatment can also alter the resin through the loss of volatile components and chemical reactions involving functional groups.
These effects can change the glass transition temperature independently or in combination.
The investigation therefore demonstrates why both composition and processing history must be considered when comparing natural resin materials.
The reported values are specific to these investigated samples, not universal values for spinifex resin.
Question 3
The Ngarrindjeri Peoples of the Murray River region are documented as using grass-tree resin mixed with sand to attach quartz tips to spears.
The Yidinji people are also documented as combining grass-tree resin with other materials, including native bee wax and mineral substances, to produce an adhesive cement.
Explain how these additional materials can influence the properties of the final adhesive.
In your response, distinguish between adhesion and cohesion, and explain why adding more mineral filler does not necessarily produce a stronger adhesive.
Solution 3
Additional materials can modify the stiffness, hardness, flow behaviour, and internal strength of the resin composite, but more filler does not automatically produce a stronger bond.
The grass-tree resin forms the main adhesive material.
Mineral particles such as sand act as fillers. They can restrict molecular movement within the resin and alter the hardness and mechanical behaviour of the composite.
Other components, such as beeswax, can modify flexibility and thermal behaviour.
The precise effects depend on the materials and their proportions.
It is important to distinguish two types of strength.
- Adhesion describes the attraction between the resin and the surfaces being joined.
- Cohesion describes the internal strength of the resin composite itself.
Adding mineral particles may improve hardness or change the flow characteristics of the adhesive. However, excessive filler can interrupt the continuous resin phase.
This may reduce the ability of the adhesive to hold together internally.
There is also a difference between making a material harder and making it more adhesive. A harder composite does not necessarily form better contact with the surfaces being joined.
The best composition depends on the intended application, not simply on maximising the amount of filler.
Question 4
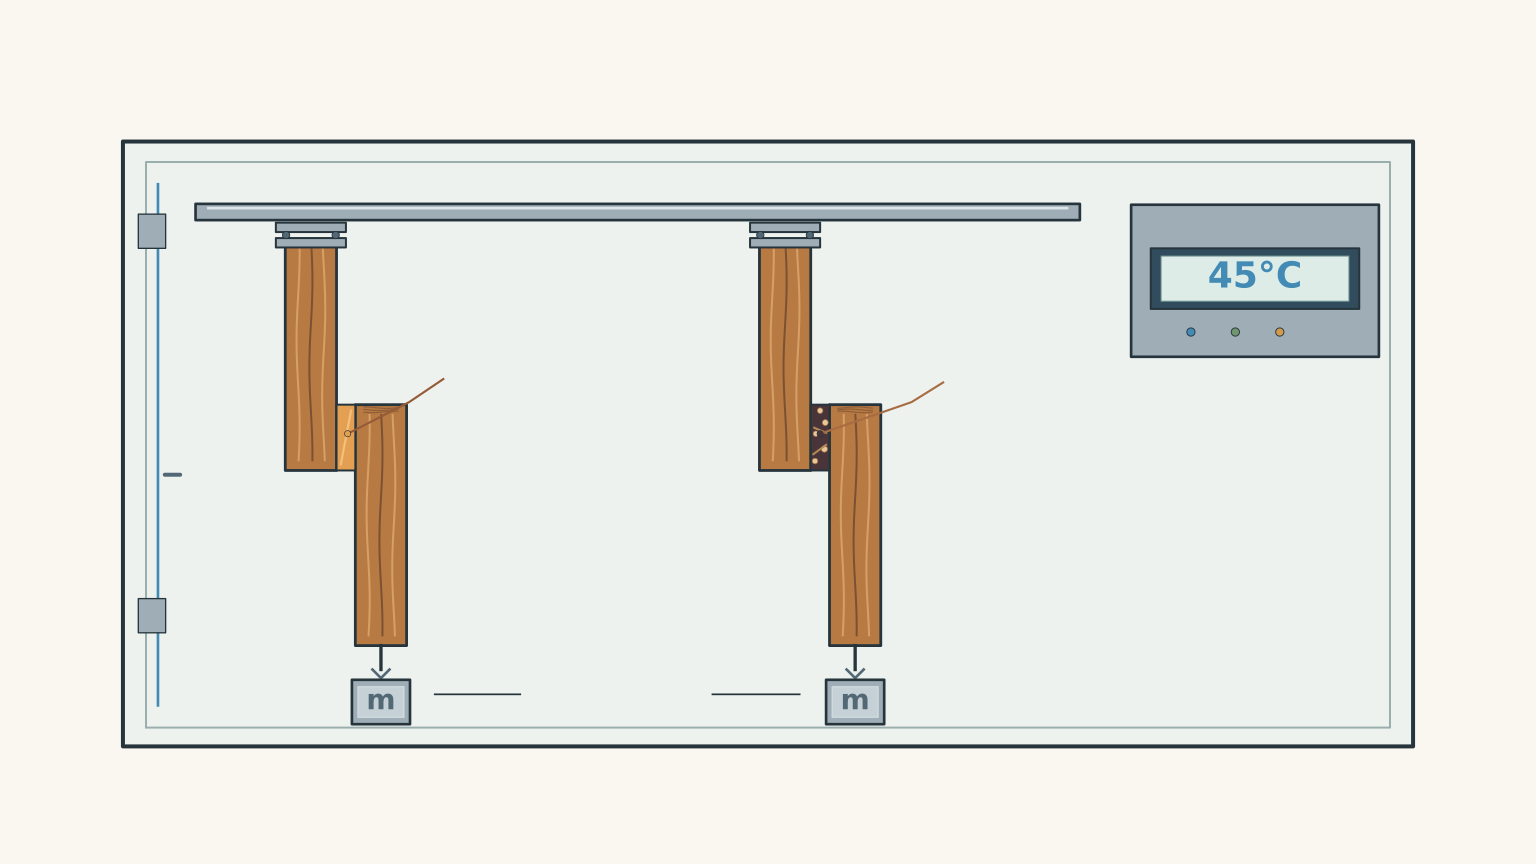
An engineer must select an adhesive for a wooden joint that will experience a temperature of 45°C for several hours under a constant load.
Two candidate materials are available:
- Adhesive A: An EVA hot-melt adhesive with a tested maximum continuous service temperature of 55°C.
- Adhesive B: A plant-resin composite with a measured glass transition temperature of 35°C.
Assume both adhesives have comparable initial bond strength and form equally effective bonds with the wood.
(a) Which adhesive would be the more appropriate choice for the stated conditions?
(b) Explain your decision using the molecular behaviour of each material.
(c) Would the same reasoning necessarily lead to the same choice if the joint operated at 20°C?
Solution 4
Adhesive A, the EVA hot-melt adhesive, is the more appropriate choice for the stated 45°C operating conditions, based on the information provided.
(a) Select the adhesive.
The EVA adhesive has a tested maximum continuous service temperature of 55°C.
The operating temperature of 45°C is below this limit.
The plant-resin composite has a glass transition temperature of 35°C, meaning the operating temperature is above its glass transition temperature.
(b) Explain the molecular behaviour.
At 45°C, the plant-resin composite is above its glass transition temperature.
Its molecular segments have increased mobility, allowing greater deformation under sustained loading.
This creates a potential risk of creep.
Creep is the gradual deformation of a material under a constant applied load.
The EVA adhesive, in contrast, is operating below its stated continuous service temperature.
Based on the supplied performance information, it is therefore the more suitable choice.
However, being below its service temperature does not mean the EVA adhesive is completely unaffected by heat. Its performance still depends on its formulation and the conditions of use.
(c) Consider a lower operating temperature.
At 20°C, the plant-resin composite is below its glass transition temperature.
It is therefore expected to behave in a relatively rigid, glassy manner.
The temperature-related disadvantage identified at 45°C is no longer present.
Consequently, the glass transition temperature alone would not justify rejecting the plant resin at 20°C.
Other factors, including impact resistance, substrate compatibility, moisture exposure, and long-term ageing, would need to be considered.
This demonstrates an important principle: an adhesive must be selected for its operating environment, not simply because it is a natural or synthetic material.
Question 5
A materials scientist investigates a plant-resin composite containing mineral filler.
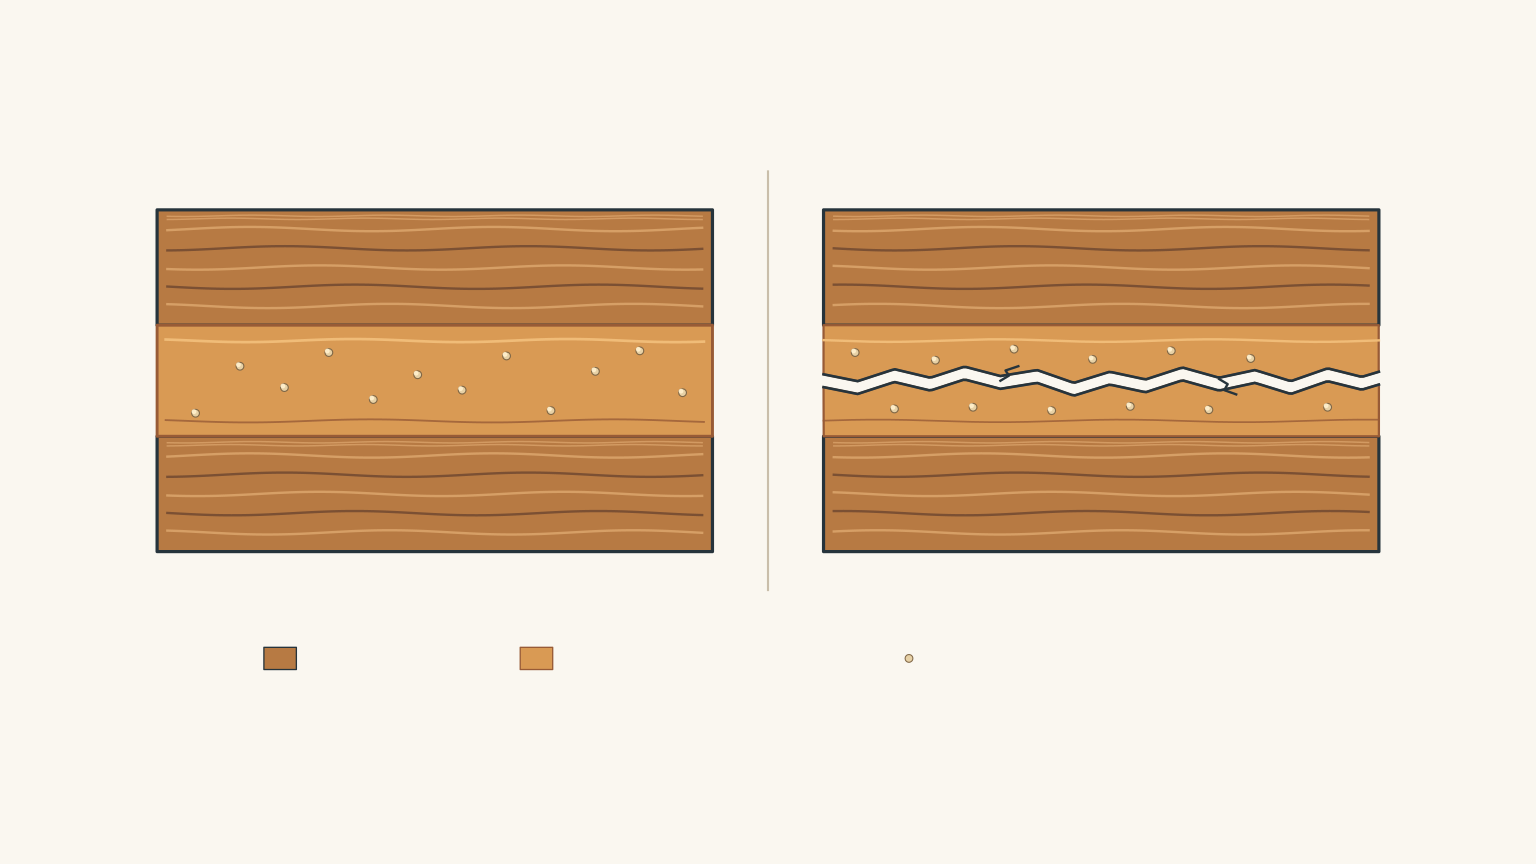
Two specimens are prepared from the same resin batch. They have the same mineral filler fraction and are tested using identical wooden surfaces.
The following observations are recorded:
| Property | Initial specimen | After three prolonged heating cycles |
|---|---|---|
| Midpoint glass transition temperature | 8°C | 40°C |
| Mineral filler fraction | Unchanged | Unchanged |
| Test temperature | 25°C | 25°C |
| Failure location | No cracking | Crack through the adhesive layer |
The post-heating specimen leaves resin residue on both wooden surfaces, indicating that the crack passed through the adhesive rather than separating cleanly at the wood-resin interface.
A student argues:
“The resin must simply have softened when heated and hardened again when cooled. Since the mineral filler fraction did not change, the material should return to its original properties.”
Evaluate this argument.
Your response should:
(a) Compare the expected physical behaviour of the two specimens at 25°C.
(b) Explain how the glass transition temperature could increase even though the mineral filler fraction remains unchanged.
(c) Explain why cooling cannot necessarily restore the original properties.
(d) Identify the type of adhesive failure observed and explain how it relates to the material’s internal structure.
Solution 5
The repeatedly heated specimen is expected to be more glass-like and brittle at 25°C, and the observed fracture is cohesive failure. The student’s argument incorrectly assumes that every change caused by heating is reversible.
(a) Compare the physical behaviour.
For the initial specimen:
\[ 25^\circ\mathrm{C}>8^\circ\mathrm{C} \]
The operating temperature is above its glass transition temperature.
The resin is therefore expected to have relatively high molecular mobility and more rubber-like behaviour.
For the repeatedly heated specimen:
\[ 25^\circ\mathrm{C}<40^\circ\mathrm{C} \]
The operating temperature is below its glass transition temperature.
The material is therefore expected to behave in a more rigid, glass-like manner.
This makes it more susceptible to brittle fracture under appropriate loading conditions.
(b) Explain the increase in glass transition temperature.
The mineral filler fraction remains unchanged, so the change cannot be explained simply by adding more filler.
Instead, the thermal history of the resin must be considered.
Two important mechanisms can contribute.
First, heating can cause volatile, low-molecular-mass components to leave the resin.
These components can act as plasticisers, increasing molecular mobility.
When they are lost, the remaining material may become less mobile, increasing its glass transition temperature.
Second, heating can promote reactions between functional groups within the resin.
These reactions can form additional crosslinks between molecular components.
Crosslinking restricts molecular movement and can increase the glass transition temperature.
Both processes provide plausible explanations for the observed change.
(c) Explain why cooling cannot restore the original properties.
The student is correct that cooling reduces molecular mobility and allows the material to become rigid again.
However, this only reverses the physical component of the heating process.
It cannot automatically reverse chemical changes.
For example:
- Volatile components that have escaped cannot be restored simply by cooling.
- Chemical crosslinks formed during heating do not disappear merely because the material becomes cold.
- Thermal degradation can permanently change the chemical structure and mechanical properties.
Therefore, the material after repeated heating may have a different molecular structure from the original specimen.
The heating-and-cooling process is not necessarily completely reversible.
(d) Identify the failure mechanism.
The observed fracture is cohesive failure.
The crack passes through the adhesive itself rather than separating the adhesive from the wooden surfaces.
This indicates that the internal strength of the adhesive has become the limiting factor.
The increased glass transition temperature provides a possible explanation for the greater brittleness of the repeatedly heated specimen.
Its more restricted molecular mobility means it may be less capable of deforming to accommodate stress.
The key misconception is assuming that a material which behaves like a thermoplastic must remain indefinitely reusable through repeated heating and cooling.
An EVA hot-melt adhesive is designed to set through a physical process without a chemical curing reaction. A complex plant-resin mixture can behave differently because heating may also change its chemical composition and molecular structure.
This is why the two materials can display similar softening and hardening behaviour without having identical chemistry.
07Sources and cultural attribution
The cultural examples in this resource are drawn from publicly available, community-attributed educational material and published research. They are specific examples, not a claim that all Aboriginal communities use the same plants, materials, or techniques.
Community knowledge and cultural sources
- Ngaparrtji Ngaparrtji Two-way Science Initiative – Western Australian Department of Education. Includes Yarnangu knowledge shared by Merna Green and local Rangers, translated by Lizzie Ellis, and prepared by Merna Green, Jodi Doyle, and Taylah Hill. The resource explicitly recognises the cultural and intellectual property of the relevant knowledge holders and language groups.
- Spinifex – Parks Australia, Uluṟu-Kata Tjuṯa National Park. Documents Aṉangu use of spinifex and the plant’s cultural significance.
- Bush foods and tools – Parks Australia. Describes Aṉangu use of kiti and its applications.
- The First Scientists – Common Ground, by Corey Tutt. A publicly attributed account by a Kamilaroi author that discusses Yidinji grass-tree resin and other First Nations innovations.
- Australian Curriculum: Science Teacher Background Information. Documents community-specific examples involving spinifex and grass-tree resins, including Ngarrindjeri and Yidinji practices.
Scientific and materials-chemistry sources
- Mondal, S., Memmott, P., Wallis, L., & Martin, D. (2012). Physico-thermal properties of spinifex resin bio-polymer. Materials Chemistry and Physics, 133, 692-699. https://doi.org/10.1016/j.matchemphys.2012.01.058.
- Resin: an essential piece of kit – Queensland Museum. Discusses the uses and material properties of selected Australian plant resins.
- Terminology and definitions for plastic packaging recycling – FEICA. Provides information about thermoplastic EVA hot-melt adhesives and physical setting.
- Adhesives 101: The Basic Composition of Hot Melts – H.B. Fuller. Explains the functions of polymers, tackifiers, plasticisers, and antioxidants.
- How Does Adhesion Work? – 3M Australia. Explains molecular attraction and mechanical interlocking in adhesive bonds.
09Where this chemistry leads next
The most useful idea from this comparison is that a material’s properties depend on both its molecular structure and how it has been processed.
A natural resin can contain many different compounds, while a synthetic adhesive can contain a defined polymer combined with carefully selected additives. Both can be designed or modified to achieve particular physical properties.
The next important comparison is between thermoplastic and thermosetting polymers.
An EVA hot-melt adhesive can be softened again because it sets physically. An epoxy adhesive, on the other hand, develops a crosslinked molecular network through chemical reactions during curing. Reheating it does not simply reverse that process.
Understanding this difference will help you connect polymer structure, intermolecular forces, chemical reactions, and material durability across the HSC Chemistry course.
For a closer look at how synthetic polymer structures influence their properties, continue with tutorgum’s Polypropylene: Addition Polymerisation, Structure and Properties.